
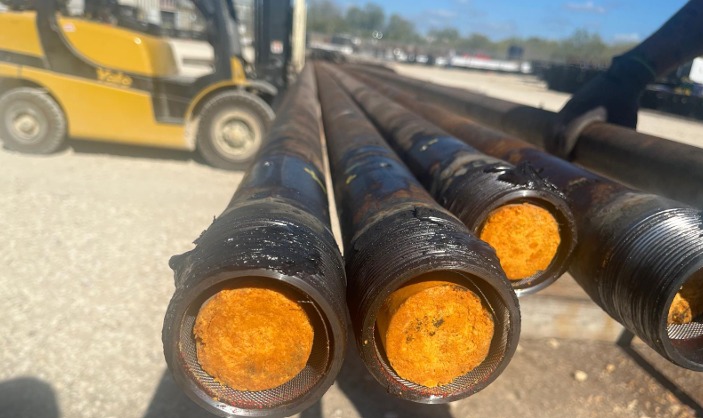
Production optimization
RYTE Production Chemistry
Field reference · Permian Basin (Scale Control)
Problem & challenge
Scale and related deposits were limiting pump and motor life, driving frequent chemical treatments and higher operating cost.
Objective
- Deliver long-duration downhole chemical protection against scale without repeated interventions.
Solution
RYTE microencapsulated chemistry was deployed in tubulars for autonomous, controlled release across the treatment interval.
Result
305 days treatment duration, zero scale on pump and motor stages, and an estimated 29% cost reduction.
Related case histories
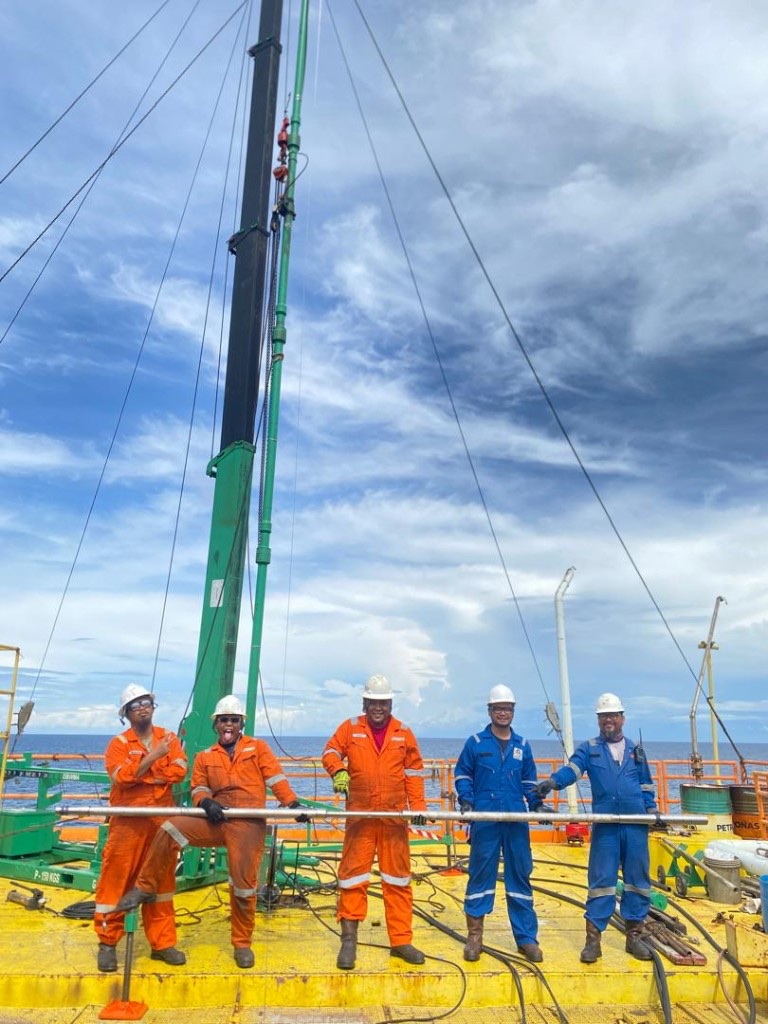
Field I through-tubing gas lift optimization
Hibiscus Petroleum · Field I, North Sabah
A super charged gas lift showed improved production, more stable well performance and better gas injection efficiency.
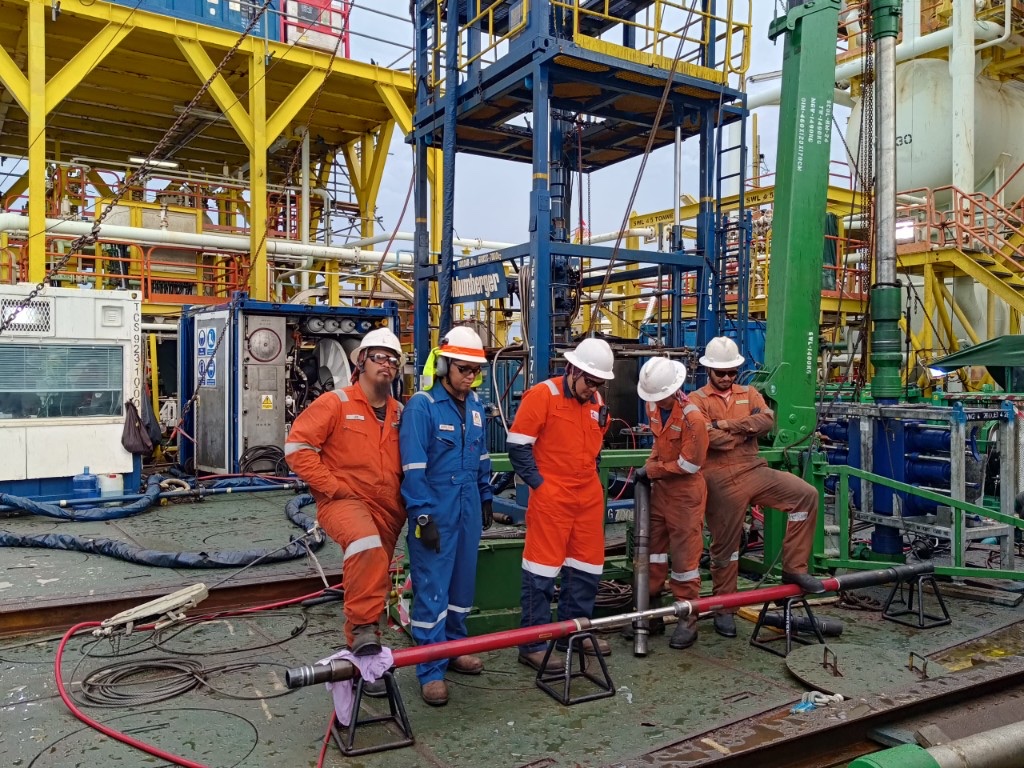
Field J through-tubing gas lift optimization
Hibiscus Petroleum · Field J, Sabah Waters
A super charged gas lift showed improved production, more stable well performance and better gas injection efficiency.
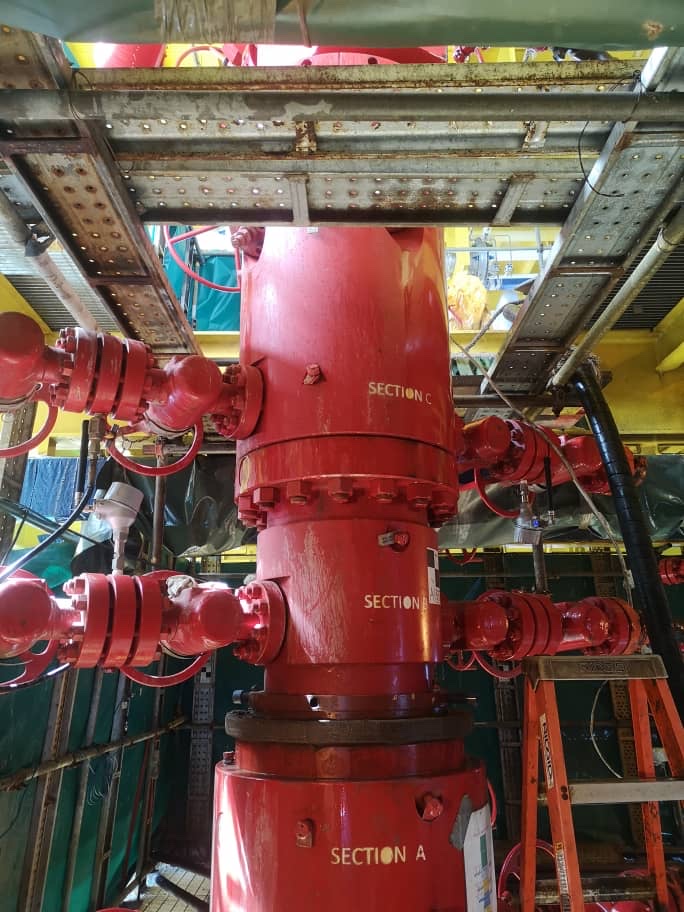
Field L remote well monitoring during infrastructure blackout
SapuraOMV · Field L, Offshore Sarawak
Continuous well pressure visibility was maintained throughout the blackout period, giving the customer reliable remote access to critical well data without permanent platform power.